 Watch video0:23
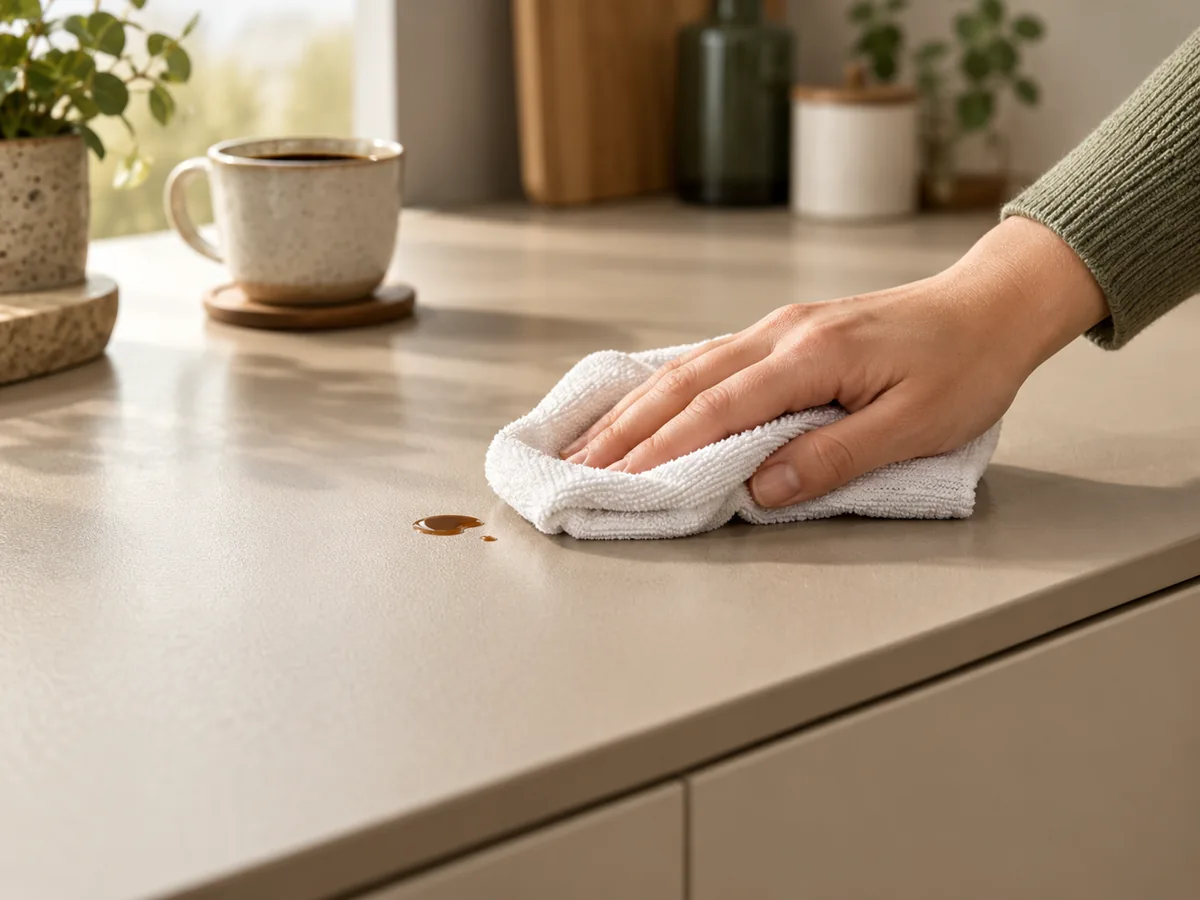
Easier everyday cleaning
Laboratory records report no visible change after wiping six food and cosmetic stains held at 25°C for 24 hours. Pen and marker results vary.
Read the cleaning conditions →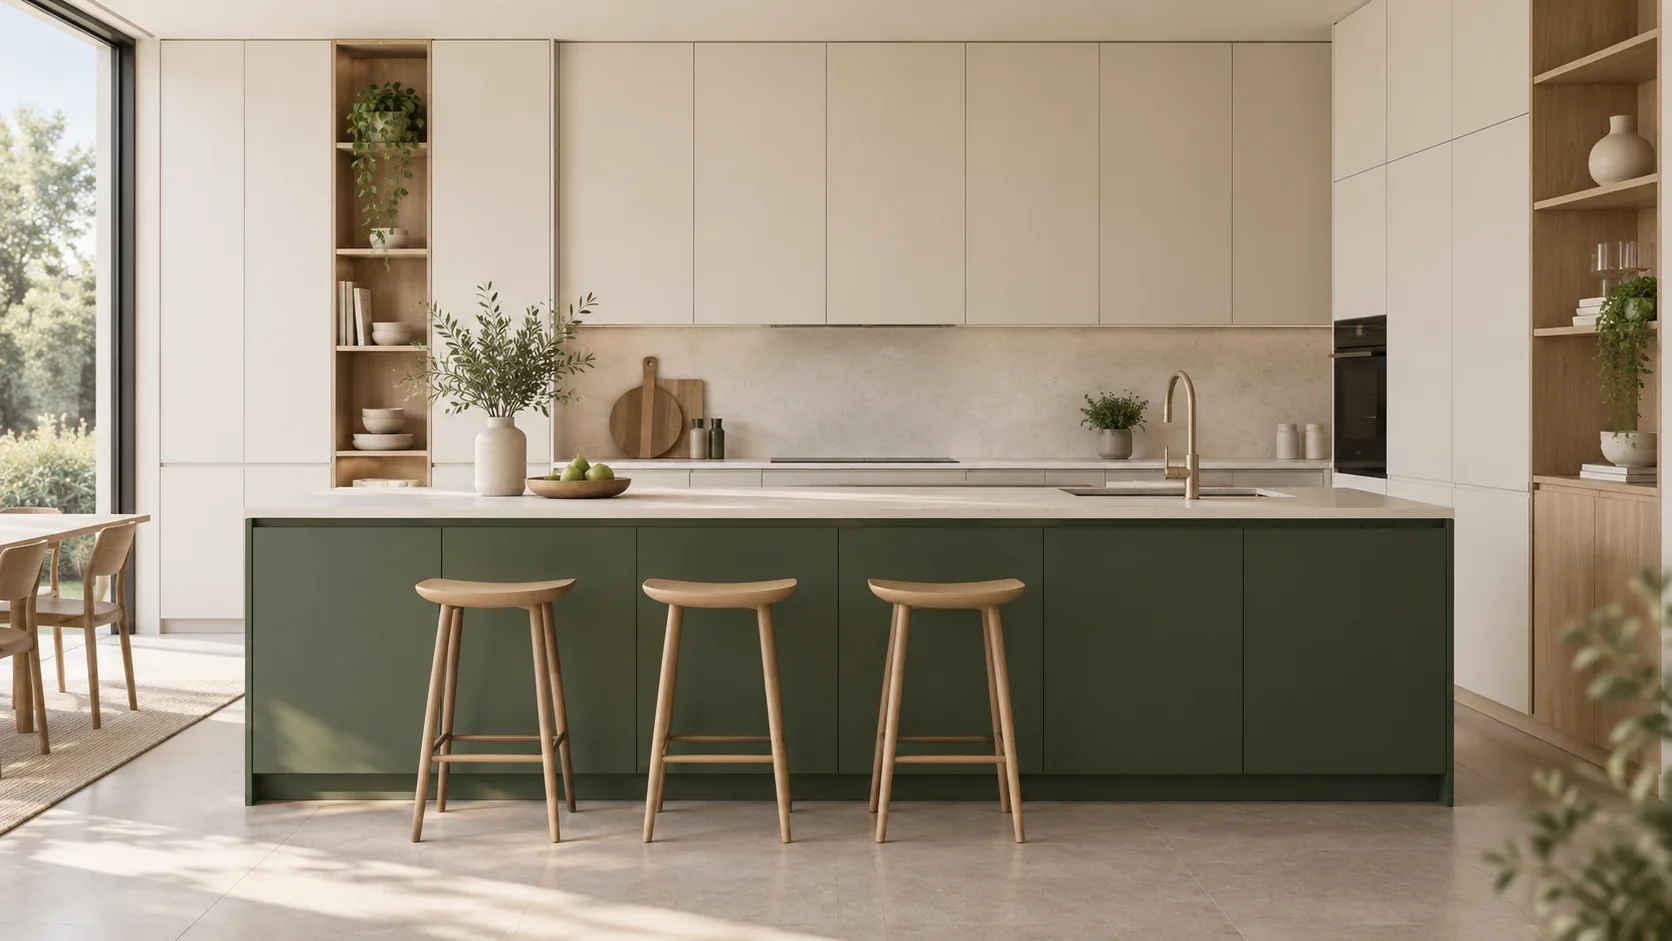
FURNITURE DECORATIVE FILM
Puremorfilm is a Chinese manufacturer of silicone decorative film and silicone laminated panels, with a silicone functional surface on a PET support film. We supply rolls without a self-adhesive backing for PUR flat lamination, or laminated panels quoted per project, for furniture fronts, cabinet doors, wall panels and other vertical or low-wear surfaces; neither supply form is suitable for floors, countertops or stovetops.
2H scratch-tested · 0 added formaldehyde · Cigarette-burn resistant
MATERIAL COMPARISON
A new generation of PVC-free furniture film brings silicone’s leather-like touch and easy-clean surface to furniture design. See how it compares with PVC thermofoil, melamine and HPL in touch, everyday care and surface performance. For a closer look at material choices, explore kitchen cabinet materials or compare wood veneer and laminate.
| What you compare | PuremorfilmSilicone film | PVC thermofoil | Melamine faced board | HPL | Printed PP film |
|---|---|---|---|---|---|
| Touch and feel | Soft, skin-like matt touch | Finish-dependent; soft-touch grades exist | Hard resin-faced surface | Hard, dense laminate | Smooth, thin plastic feel |
| Everyday cleaning | 24-hour stains wipe clean | Easy-clean grades available | Easy-clean sealed surface | Strong everyday stain resistance | Depends on topcoat |
| Scratch resistance | 2H: no obvious scratches | Depends on protective topcoat | Hard-wearing; check surface class | Hard-wearing; check EN 438 grade | Topcoat-dependent; soft films mark |
| Surface wear | 2,000 cycles; slight mattification | Wear-layer dependent | Grade-dependent wear class | Abrasion-rated grades available | Wear resistance: topcoat-dependent |
| Heat stability | 0.06%/0.10% change, 100°C/600-min test | Heat-sensitive film and adhesive system | Grade and exposure-time dependent | Heat-resistant grades available | Thermoplastic; check heat rating |
| Cigarette contact | Cigarette-burn-resistant film | Request grade-specific contact result | Check the surface rating | Resistant grades available | Request grade-specific contact result |
| Ageing over years | No DOP; resists embrittlement | Formulation-dependent plasticizer migration | Stable; grade-dependent appearance | Stable resin laminate | Stable; topcoat may wear |
| Surface material | PVC-free; no added formaldehyde | PVC-based; formulation-dependent additives | Resin paper; low-emission grades exist | Resin laminate; low-emission grades exist | PVC-free polymer; check coatings |
| Profiles and edges | Flat lamination with PUR adhesive | 3D thermoforming of suitable grades | Flat panels; edge banding needed | Flat bonding / grade-specific postforming | Flat lamination and wrapping |
Silicone vs PVC thermofoil
| Property | Silicone film | PVC thermofoil |
|---|---|---|
| Touch and feel | Soft, skin-like matt touch | Finish-dependent; soft-touch grades exist |
| Everyday cleaning | 24-hour stains wipe clean | Easy-clean grades available |
| Scratch resistance | 2H: no obvious scratches | Depends on protective topcoat |
| Surface wear | 2,000 cycles; slight mattification | Wear-layer dependent |
| Heat stability | 0.06%/0.10% change, 100°C/600-min test | Heat-sensitive film and adhesive system |
| Cigarette contact | Cigarette-burn-resistant film | Request grade-specific contact result |
| Ageing over years | No DOP; resists embrittlement | Formulation-dependent plasticizer migration |
| Surface material | PVC-free; no added formaldehyde | PVC-based; formulation-dependent additives |
| Profiles and edges | Flat lamination with PUR adhesive | 3D thermoforming of suitable grades |
Silicone figures refer to the recorded film specimens. Other columns describe typical material categories; grades and test methods vary. View silicone test conditions. Film, adhesive and core-board performance are assessed separately.
Compare a physical sample against your current finish.
Request a Comparison SampleFinish complaints can start after delivery on cabinet doors, furniture fronts and exposed panel edges. If one of these sounds familiar, the PVC-free answer is just below.
Coffee rings, oil and marker turn routine cleaning into scrubbing — and scrubbing dulls the finish even faster.
See cleaning performance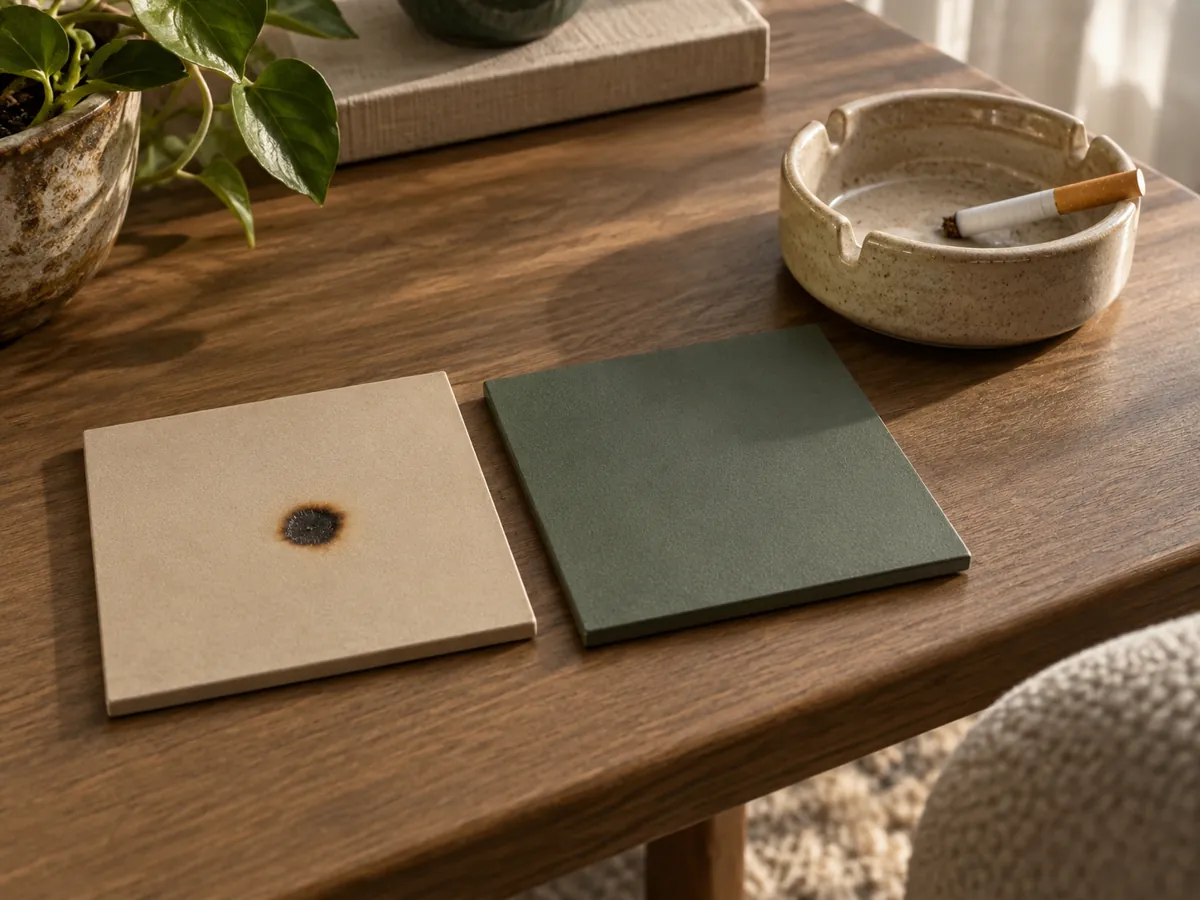
Heat damage on a furniture surface can require panel replacement. Keep our film off countertops, desktops used as worktops and stovetops; a film test does not approve those uses.
See burn resistance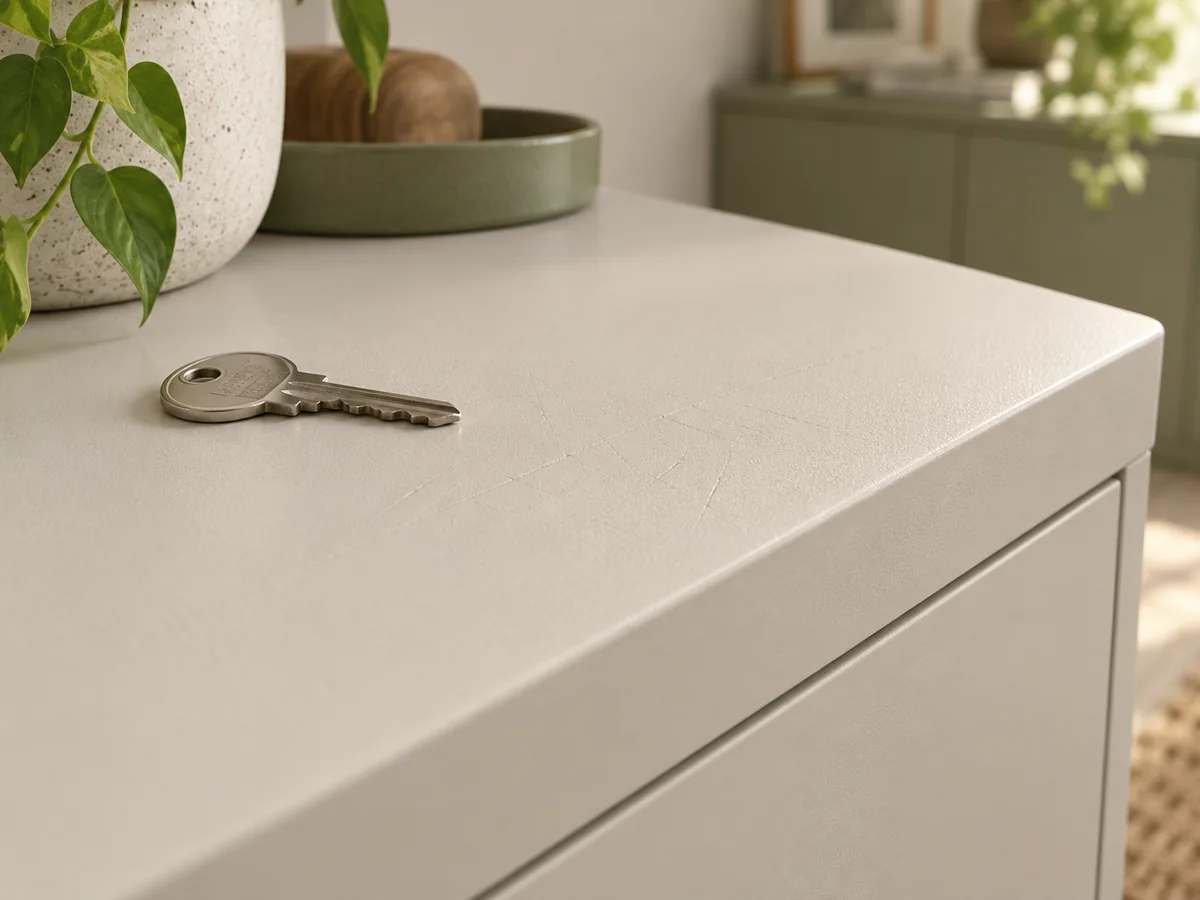
Keys, toys, chair backs and daily handling can scratch cabinet doors and furniture fronts.
See scratch resistanceDoors next to ovens and dishwashers soften, bubble or peel — the classic thermofoil cabinet complaint.
Check heat and bond performance
After a few years, light colours can turn yellow and films can go brittle and crack — just when customers expect the furniture to last. PVC films can also turn brittle as plasticizers migrate out.
See long-term stability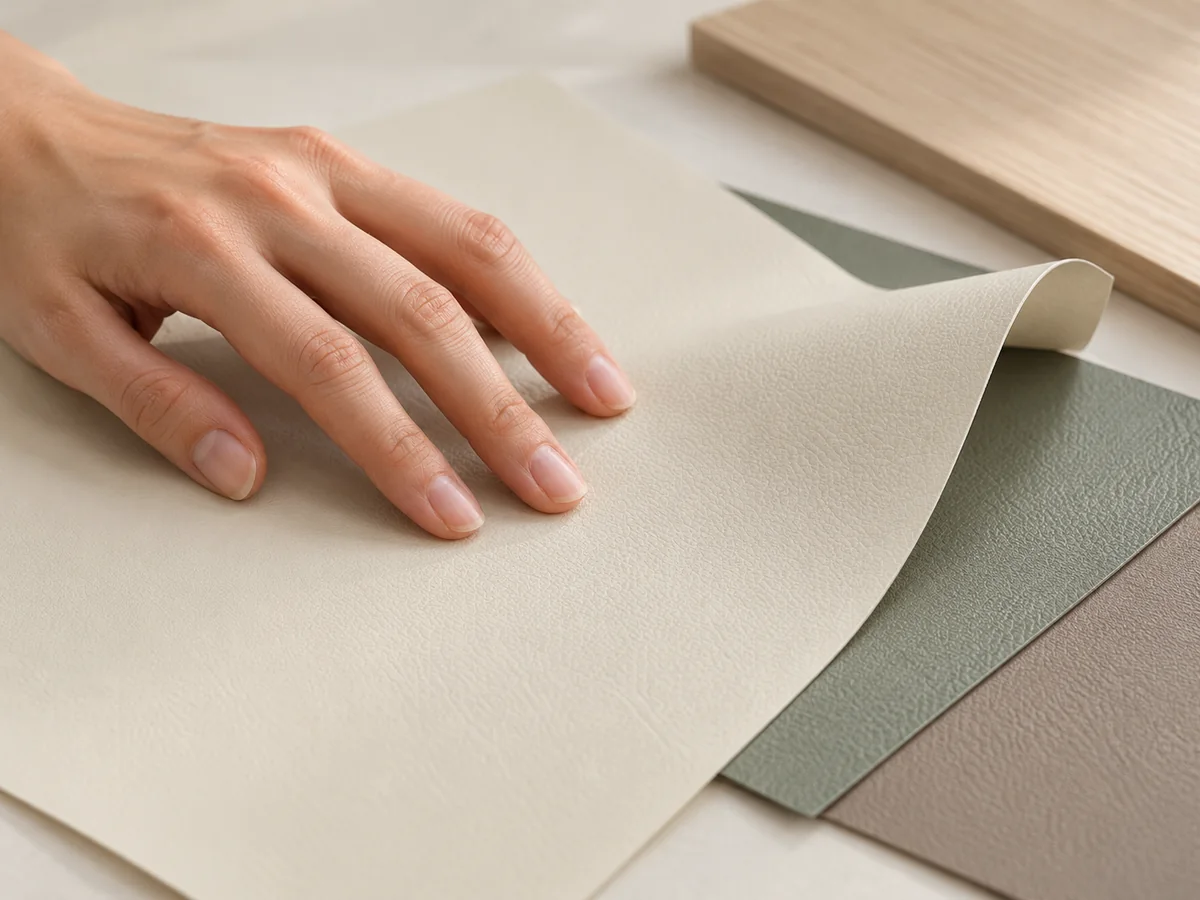
A finish that photographs well but feels thin or plasticky in the hand undercuts the price you are asking.
Choose by look and touchTell us which problem costs you the most — we will match a sample to it.
Discuss My Surface ProblemStart with cleaning and cigarette contact, then evaluate the matching film on your own furniture construction.
Watch video0:23Laboratory records report no visible change after wiping six food and cosmetic stains held at 25°C for 24 hours. Pen and marker results vary.
Read the cleaning conditions →Watch video0:32Request the result, contact time and specimen details for your chosen grade. Cigarette-burn resistance and flame retardancy are evaluated separately.
Request Burn Test Details →Evaluate the surface on samples before specifying it.
Request Samples for EvaluationReview production capability, then agree the quality checks for your order. Watch the factory video
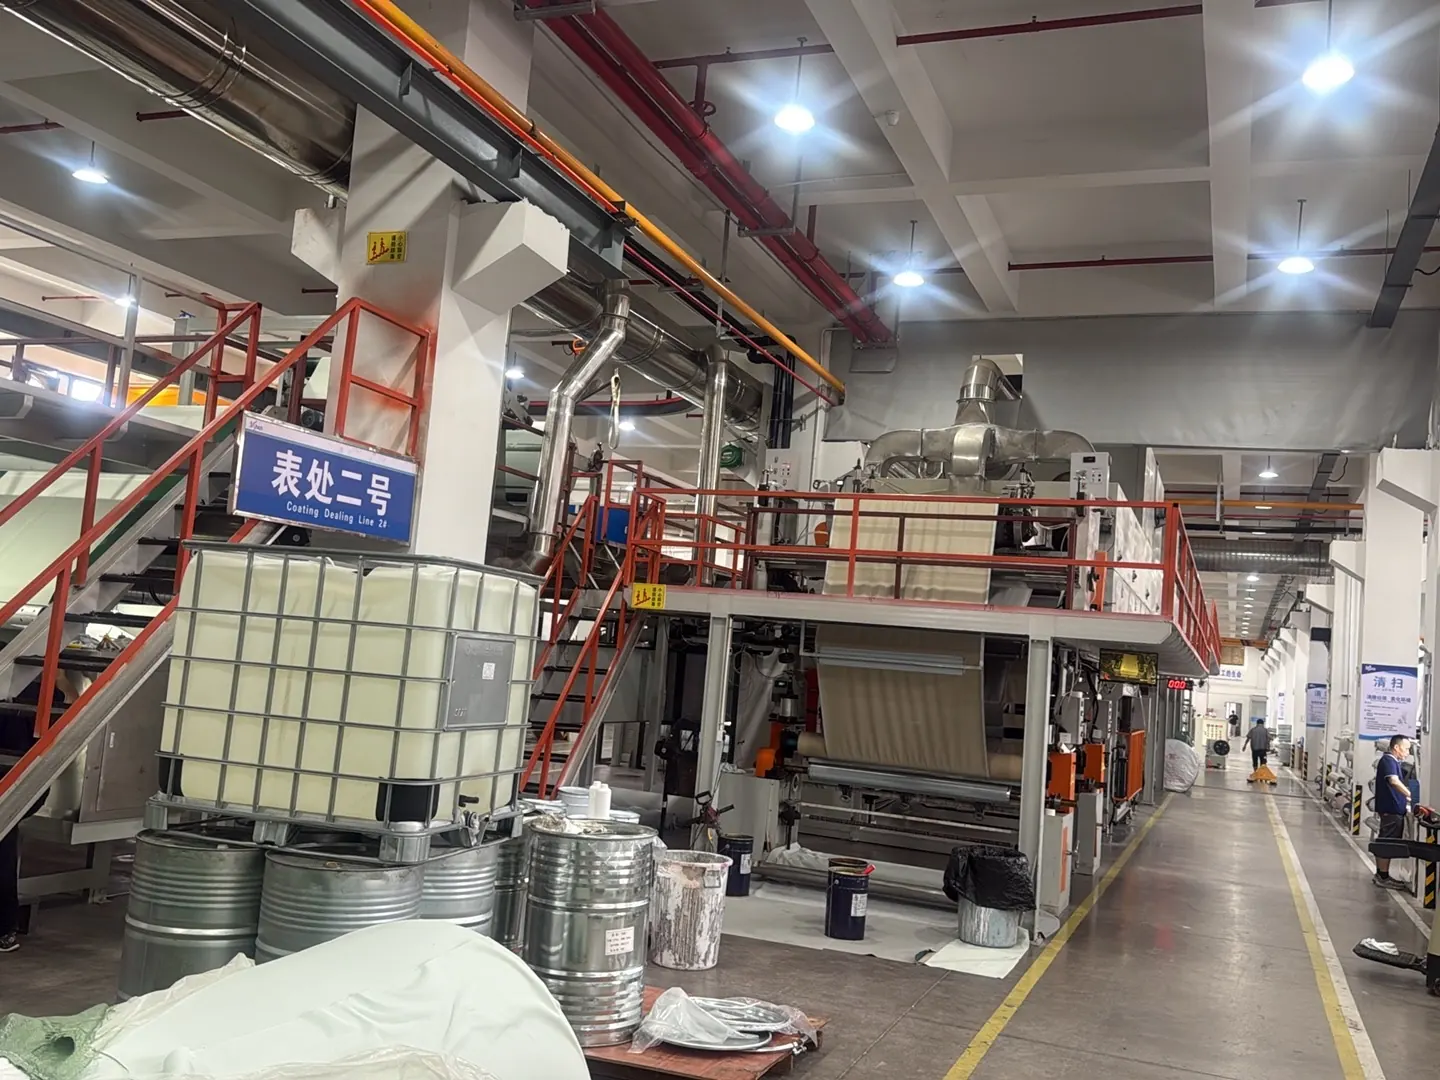
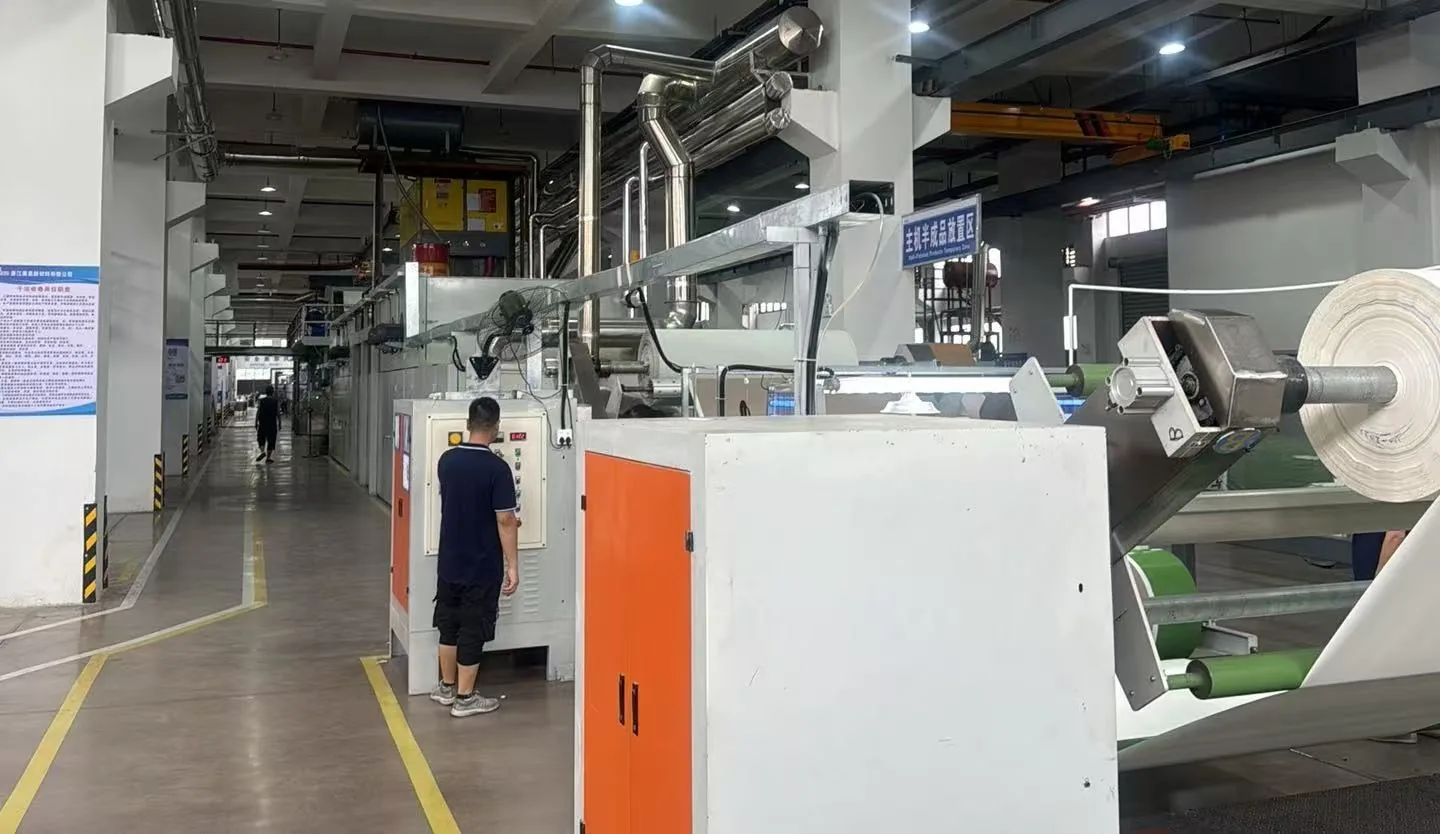
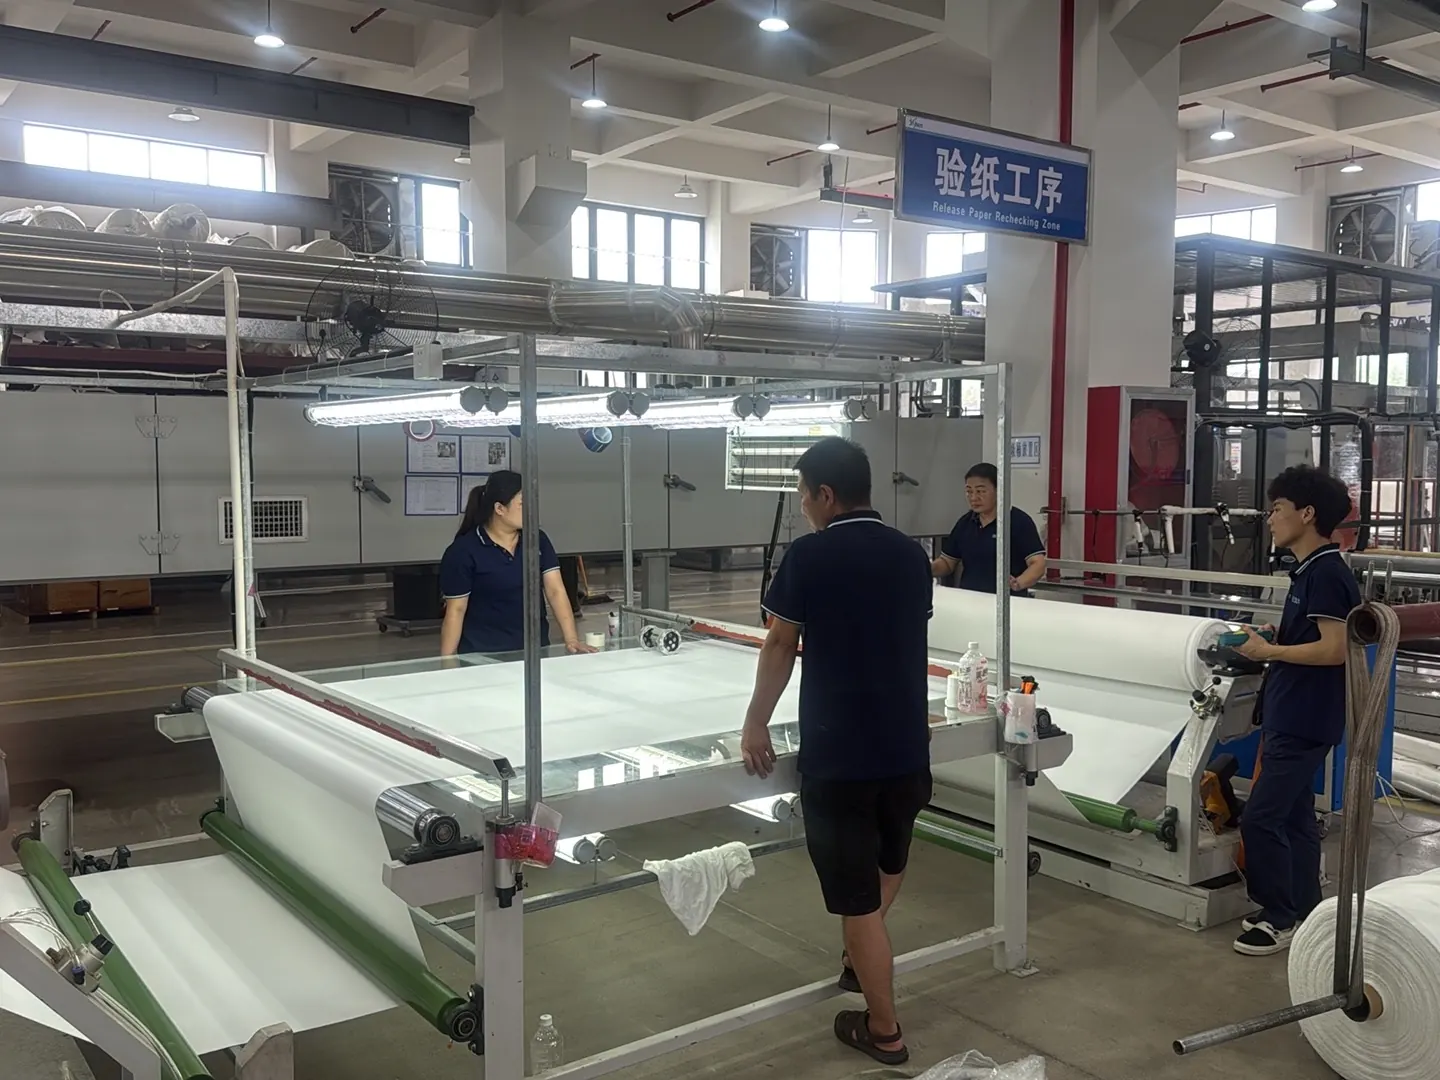
Explore the coating, curing and roll-finishing stages. See our operating production lines on a live video factory tour.
Agree the inspection items, tolerances and records with the approved sample before production.
Material specification, batch identity and surface condition.
Thickness, coating uniformity, colour, texture and visible defects.
Width, length, appearance and grade-specific acceptance checks.
Model, batch labels, quantity and protective packing against the order.
Confirm the approved reference sample and inspection frequency. Agree how nonconforming material is identified, held and rechecked, and which production and inspection records accompany the supplied batch. Request the applicable QC checklist for your order.
Review the production lines and discuss your inspection requirements.
Book a Video Factory Tour Request QC DetailsSelect an application to see the checks that matter before sampling and production.
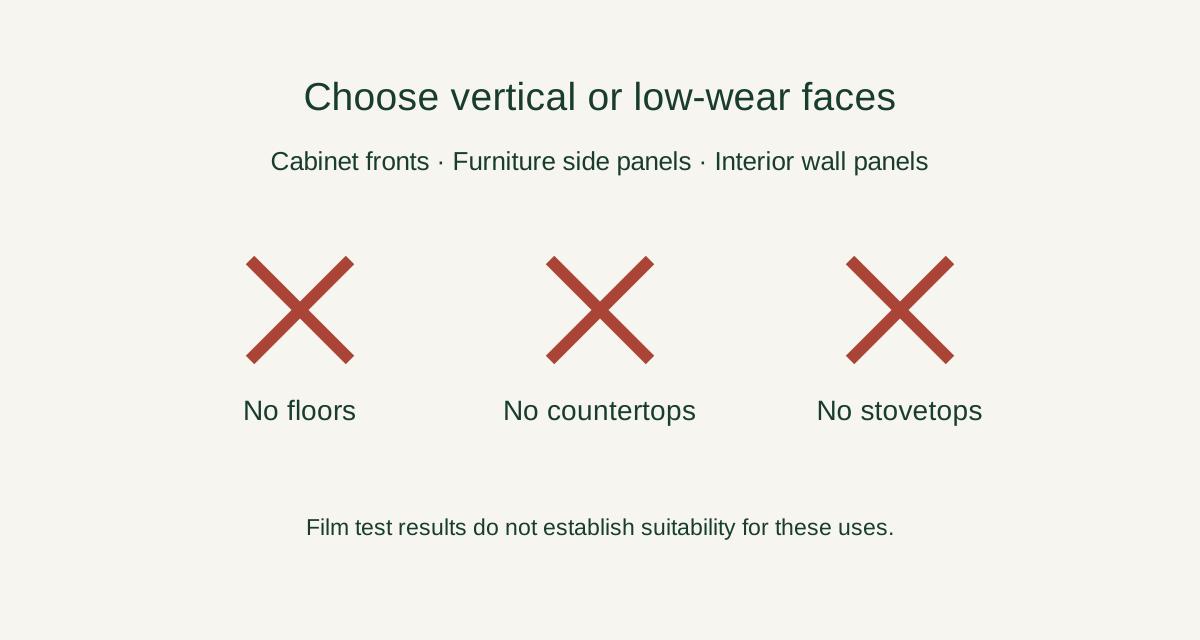
Do not specify the current film for countertops, desktops used as worktops or stovetops. Use it for vertical or low-wear furniture faces instead.
Compare colour consistency and touch on a panel sample in your chosen finish.
Evaluate the film, adhesive and board together for heat, moisture and edge performance.
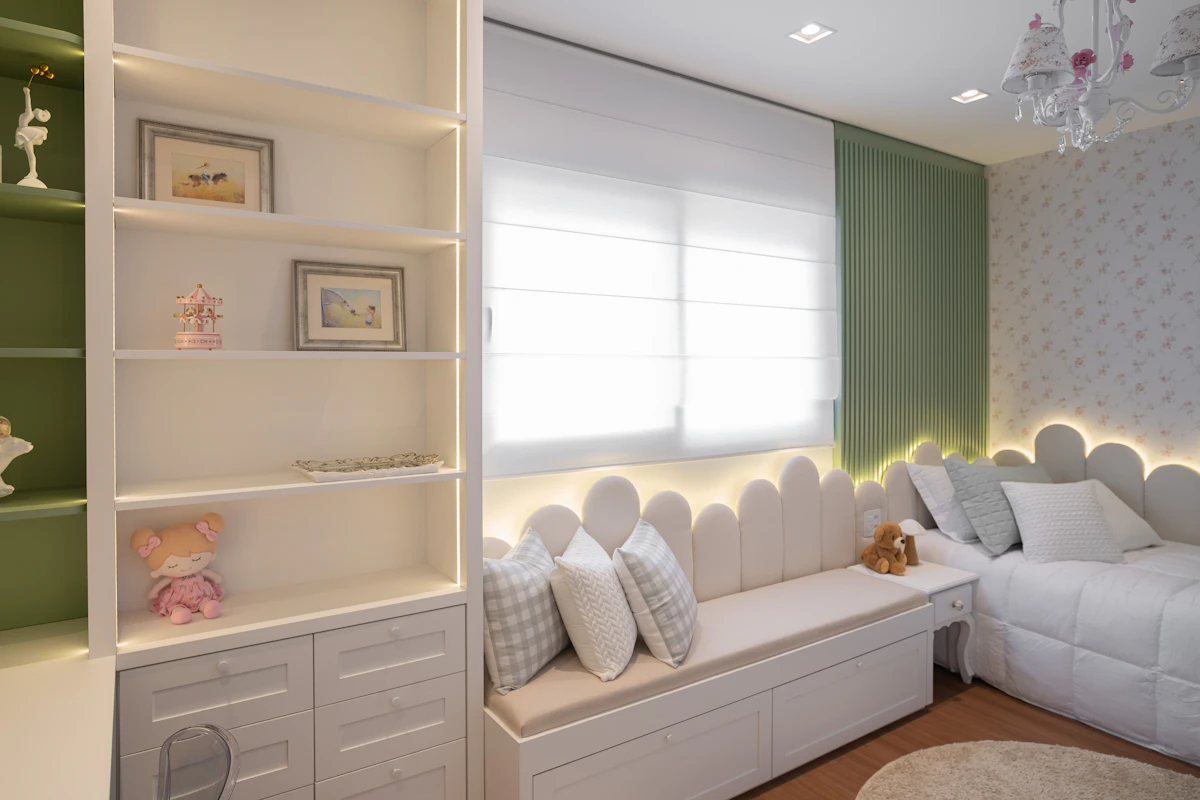
Choose a finish around handling, cleaning and the intended storage environment.
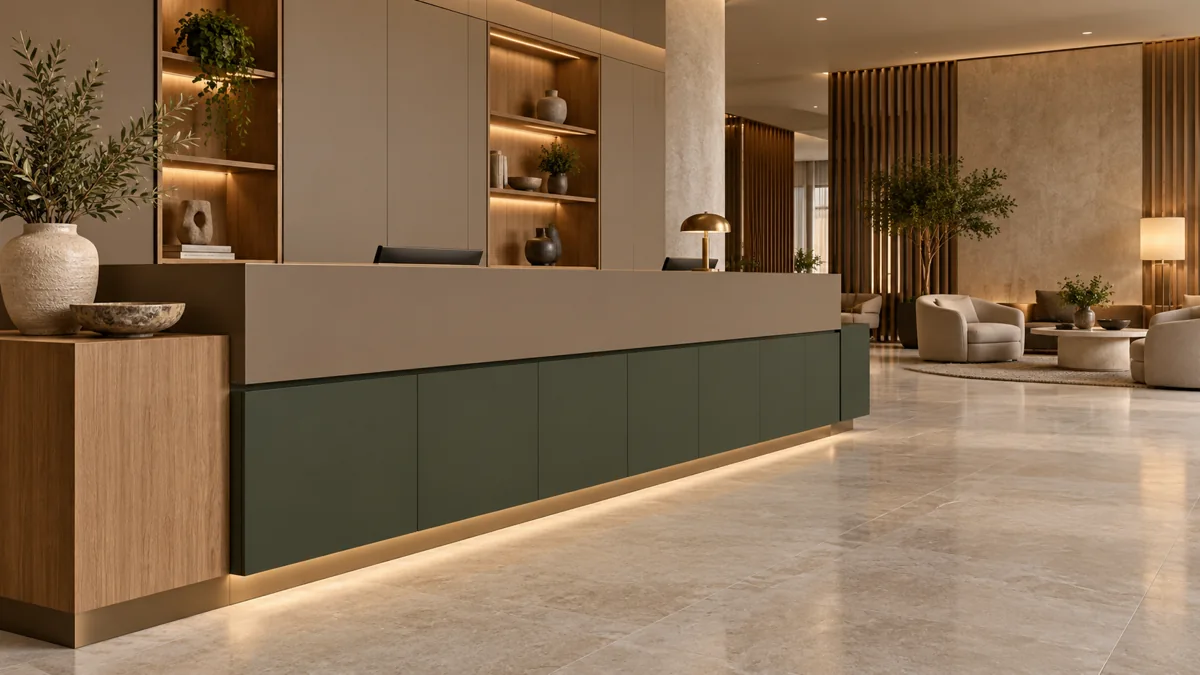
Match appearance, maintenance and project standards to the proposed furniture construction.
Need a reference for a similar application? Ask about available project references.
Discuss a Similar ProjectExplore wood grain, solid colours and leather textures. Request physical samples to compare colour, texture and touch. A panel sample also shows the finish after bonding.
For tone, grain direction and physical sample selection, explore our wood grain decorative film.
Choose a finish family and compare the actual material in your hands.
Request Colour SamplesChoose what fits your production setup. Supply combinations and tolerances are confirmed for the selected model.
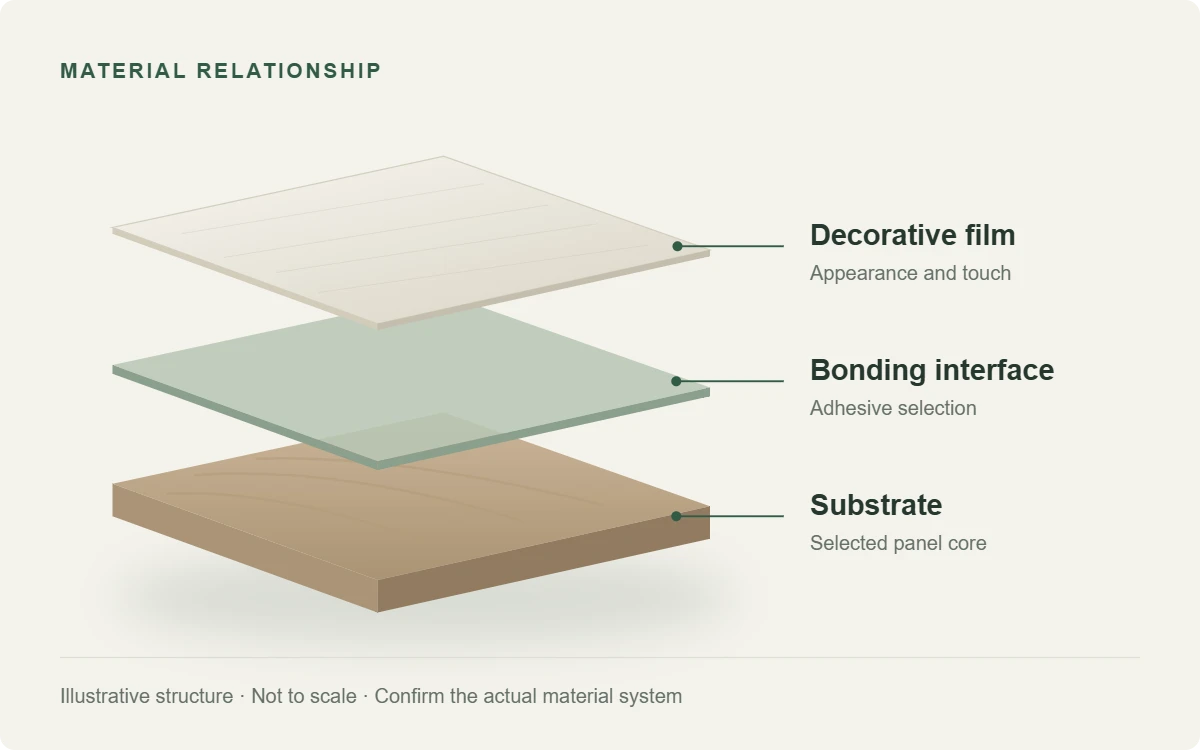
Product literature lists PET support film and development options including PC or TPU; confirm the backing for the selected grade. Gloss is approved on a physical sample. The documented 1220 × 2440 mm size is a wall-panel specification; furniture-panel size is confirmed separately.
Not sure which supply form to choose? Describe your equipment and end product.
Help Me Choose a Supply FormReview the highlights, then expand the records you need. Results apply to the stated film specimen or formulation; finished-panel requirements are confirmed by construction.
No obvious scratches
2H pencil · 500 gf · 45° · three strokes ≥20 mm. White paper summary of SGS PL02.
2,000 cycles
Slight mattification only; no concentrated scratches, exposed backing or coating peeling. CS-10 · 1,000 g per wheel · 60 rpm. SGS PL04 summary.
0.06% / 0.10%
Length / width after 100°C for 600 minutes and 14-hour room-temperature recovery. SGS PL01 summary.
Source: technical white paper V1.0 (October 2026), including SGS report summaries, laboratory records and patent worked examples. Request the original matching report for the supplied model.
| Test item | Recorded result | Test conditions | Source & scope |
|---|---|---|---|
| Pencil scratch | No obvious scratches | 2H pencil; 500 gf load; 45° angle; three strokes, each ≥20 mm. | SZIN2608002405PL02_EN 26 Aug 2026. Tested film specimen; resistance under these tool and load conditions. |
| Taber abrasion | 2,000 cycles: slight mattification only; no concentrated scratches, substrate exposure or coating peeling. | ASTM D4060-25; CS-10 wheels; 1,000 g per wheel; 60 rpm. | SZIN2608002405PL04_EN 27 Aug 2026. Surface-wear evidence for the tested film; assess against the intended wall or furniture use. |
| Thermal dimensional stability | Length change 0.06%; width change 0.10%. | 100°C for 600 minutes, followed by 14 hours at room temperature. Lab environment: 23±2°C, 50±5% RH. | SZIN2608002405PL01_EN 26 Aug 2026. Supports dimensional and processing evaluation of the tested film. |
| Tensile breaking force & elongation | A1: 216.4 N / 51% A2: 126.3 N / 67% Specimen thickness: A1 0.473 mm; A2 0.605 mm. | JIS K 6732:1996+AMD.1:2006 and client requirements; 200 mm/min; 40 mm gauge length; 23±2°C, 50±5% RH. | SZIN2608002405PL03_EN 27 Aug 2026. N is breaking force. Specimens 1 and 2 broke outside the gauge marks; those results are for reference only. |
| Test item | Recorded result | Test conditions | Source & scope |
|---|---|---|---|
| Food, drink & cosmetics | No visible change after wiping: coffee, red wine, ice cream, soy sauce, Worcestershire sauce and lipstick. | Contaminants applied to the film surface; held at 25°C for 24 hours, then wiped. | Laboratory data, white paper §6.2. Results apply to the stated exposure and wiping method; match cleaners to the supplied grade. |
| Pen & marker marks | No visible change or slight staining: ballpoint pen, water-based marker and oil-based marker. | Same recorded method: 25°C for 24 hours, followed by wiping. | Laboratory data, white paper §6.2. The recorded result varies; confirm the contaminant-specific result for the chosen film. |
| Test item | Recorded result | Test conditions | Source & scope |
|---|---|---|---|
| Internal film interlayer peel | BOPET system: ≥3 N/15 mm TPU system: ≥3.5 N/15 mm. | 180° peel; BOPET backing 125 μm and TPU backing 200 μm. | Patent worked examples 1 and 2, white paper §5.4. Internal film interface only; does not establish film-to-board adhesive strength. |
| Damp-heat ageing | No delamination or blistering. | 85°C / 85% RH for 500 hours. | Patent worked-example data, white paper §5.4. Confirm the corresponding construction for supply. |
| Thermal cycling | No delamination or blistering. | −40°C to 85°C; 100 cycles. | Patent worked-example data, white paper §5.4. Applies to the evaluated example construction. |
| Boiling-water exposure | No delamination or blistering. | Boiling water for 12 hours. | Patent worked-example data, white paper §5.4. Confirm film grade and construction. |
| Antibacterial reduction | ≥99% against Escherichia coli and Staphylococcus aureus. | Recorded for an antibacterial worked-example formulation. Confirm formulation grade and corresponding test conditions. | Patent worked-example data, white paper §9. Antibacterial performance is grade-specific; request evidence for the supplied model. |
| Surface wettability | Water contact angle approximately 108° in the worked example; stated range 100°–115°. | Worked-example surface measurement; full measurement conditions to be matched to the grade. | Patent worked-example data, white paper §6.1. A wettability measure for the evaluated surface. |
| Test item | Recorded result | Test conditions | Source & scope |
|---|---|---|---|
| Accelerated ageing | No visible change after 2,000 hours. | White paper records JIS B7753 light and water exposure testing. | Laboratory data, white paper §7.2. Confirm the original exposure program and film grade for a weathering specification. |
| Yellowing resistance | Grade ≥4. | QUV-A testing, as recorded; duration and grading details to be confirmed with the matching test record. | Laboratory data, white paper §7.2. Compare only with a matching procedure and grading scale. |
| Hydrolysis exposure | Recorded duration ≥10 weeks. | 85°C / 85% RH. | Laboratory data, white paper §7.2. Request the appearance/strength acceptance criteria for the specified grade. |
| Salt-spray exposure | Recorded duration ≥1,000 hours. | ASTM B117, as recorded in the white paper. | Laboratory data, white paper §7.2. Project acceptance criteria and the post-exposure result are confirmed separately. |
| Water staining | Class 5. | ISO 105-E01 / ASTM D1735-2021, as recorded. | Laboratory data, white paper §7.2. Confirm the grading procedure and specimen. |
| Perspiration staining | Class 5. | ISO 11641:2012 / ISO 105-E04, as recorded. | Laboratory data, white paper §7.2. Confirm the intended contact conditions and film grade. |
The film layer is described as having no added formaldehyde and a No DOP formulation. Request the matching material-safety document. For laminated panels, assess the adhesive and core separately.
Cigarette-contact results need the film grade, contact time and method. Flame-retardant performance needs the applicable standard and construction. One result does not establish the other.
Share a reference sample or design brief for a custom colour, pattern or texture. Feasibility and supply terms are confirmed before proofing.
Reference colour, wood grain or a design file, with the intended furniture application.
Describe the grain, gloss and hand feel you want to compare on a physical proof.
Discuss the required width, thickness, quantity and any packaging or labelling needs.
Design brief → Feasibility & terms → Physical proof → Approved production reference
Have a finish reference? Add it to your inquiry.
Discuss a Custom FinishShare your substrate, adhesive and equipment. Trial the proposed construction and edge treatment before a volume order; compatibility is confirmed for the selected film grade.
Send your substrate and process details — we will check the fit before you order in volume.
Submit My Substrate & ProcessEvaluate the cost of an accepted finished surface, including your processing and delivery requirements.
Grade, finish, thickness and supply form.
Adhesive, labour, line settings and yield.
Roll or panel protection and order size.
Destination, freight method and schedule.
Standard film rolls start at 500 m; laminated panels are 1220 × 2440 mm and start at 200 sheets. Unit price depends on the selected grade, specification, finish and quantity. A custom finish may require separate proofing and a different production quantity. Request a quote that states sample costs, freight, MOQ, lead time and packing.
Share what you know now; missing details can be confirmed during evaluation.
Get a Project QuoteConfirm the material and acceptance requirements first, then agree the production and delivery plan.
Choose the finish and film or panel sample for your application.
Agree the construction, specification, acceptance criteria, quantity and terms.
Confirm the production checks, batch identification and inspection records.
Agree protective packing, outgoing checks, documents and freight arrangements.
Planning guide: sample dispatch 3–5 working days; standard bulk production 15–25 days after deposit; custom patterns may add 7–10 days for proofing and approval. Confirm the actual schedule with the quote against the model, quantity and requirements. Freight transit is planned separately.
Begin with a sample set and the checks you want to run.
Start Sample EvaluationA few final checks for furniture makers and project buyers.
Yes. The surface is crosslinked silicone on a PET support film — not PVC, melamine paper or a printed PP film. It uses a No DOP formulation.
Yes. The film layer has no added formaldehyde. For laminated panels, the adhesive and core board are documented separately so your project file covers every layer.
Standard film rolls are supplied without back adhesive. Confirm the adhesive, board and lamination method for the selected grade, then trial the construction on your line. Laminated panels are an alternative when you need the film already bonded to a board.
Each burn result is tied to a named film model and the stated test conditions, including contact time and placement. Ask for the record of the model you plan to use and we will share the result with its conditions.
Not automatically. Film results describe the film. A laminated panel's fire performance depends on the film, adhesive and core board together, so it is evaluated by construction for your project.
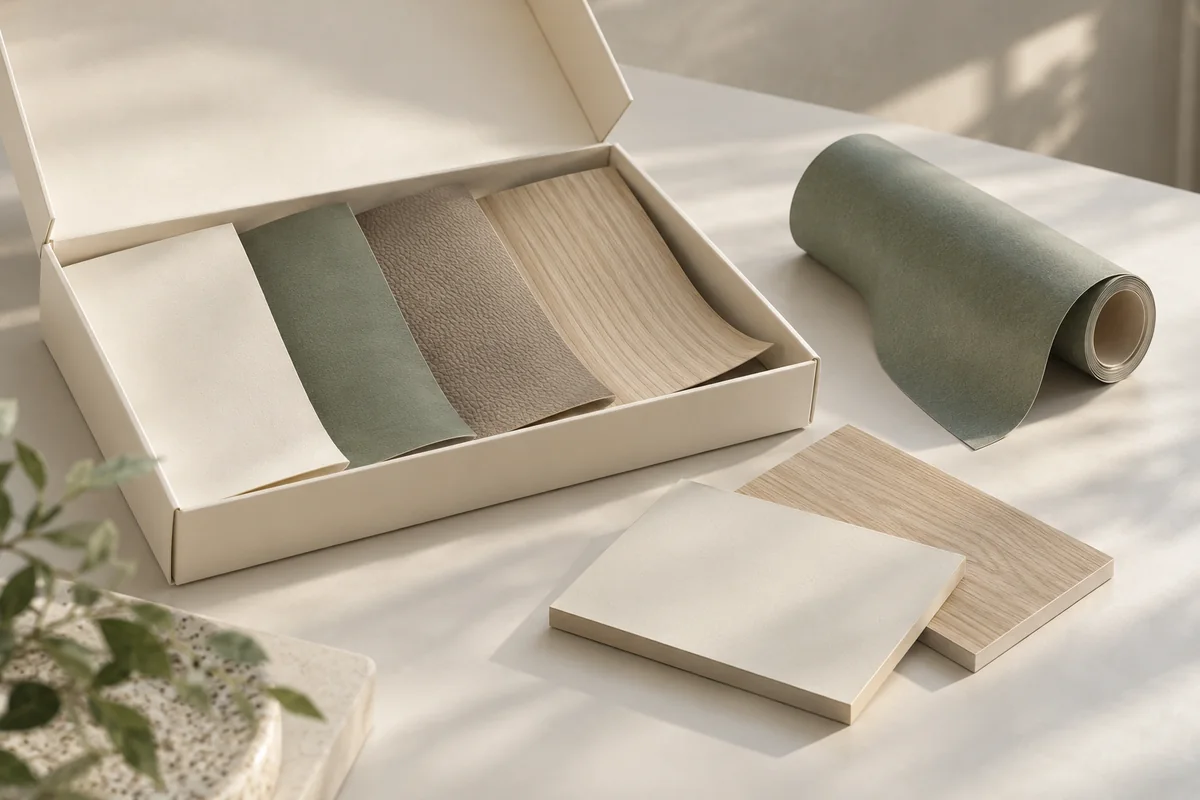
Colour swatches help you choose the look. Film samples let you test cleaning and run lamination trials on your own line. Panel samples show how the finished door or furniture panel looks and feels once the film is bonded.
Standard film rolls start at 500 m; laminated panels are 1220 × 2440 mm and start at 200 sheets. Unit price, lead time and packing are confirmed for the selected model, supply form, specification and quantity.
Have a question not covered here? Our technical team will answer it directly.
Ask a Technical QuestionChoose samples, a quote, test documents or a processing discussion. Share your application and any selected finish; only your email is required.
Thank you. We will reply by email with the samples, documents or quote you requested.
Keep browsing colours and textures